top of page


> Home
> Industries
Inorganic & Mineral Chemicals
Engineering reliable production for essential chemical industries.

Inorganic & Mineral Chemicals
Inorganic and mineral chemicals are essential to many industrial processes. We deliver engineering and EPC solutions for reliable, efficient, and compliant chemical production plants across diverse industrial sectors.

Inorganic & Mineral Chemical Categories

Salts & Brines
Sodium Chloride (NaCl)
A fundamental industrial salt used in chemical manufacturing, water treatment, food processing, chlor-alkali production, and de-icing applications.
Potassium Chloride (KCl)
Widely used in fertilizers, industrial processes, and chemical synthesis, supporting agriculture, pharmaceuticals, and specialty chemical production.
Calcium Chloride (CaCl₂)
Utilized for dust control, de-icing, moisture absorption, and as a processing aid in industrial and construction-related applications.
Magnesium Chloride (MgCl₂)
Applied in industrial processing, dust suppression, refractory materials, and as a precursor for magnesium-based chemicals.
Sodium Bromide (NaBr)
Used in water treatment, drilling fluids, pharmaceuticals, and industrial specialty chemical formulations across multiple regulated industries.
Sodium Carbonate
Essential for glass manufacturing, detergents, water treatment, and various inorganic chemical processes, commonly known as Soda Ash.

Sulfates
Aluminum Sulfate (Alum)
Commonly used as a coagulant in water and wastewater treatment, paper manufacturing, and industrial clarification processes worldwide.
Copper Sulfate Pentahydrate
Applied in agriculture, mining, water treatment, and industrial chemical formulations requiring controlled copper content and consistent product quality.
Nickel Sulfate Hexahydrate
A key raw material for electroplating and lithium-ion battery cathode production in energy storage and electric vehicle applications.
Ferrous Sulfate (FeSO₄)
Used in water treatment, agriculture, pigments, and chemical processes requiring iron-based compounds with stable performance and controlled purity.
Zinc Sulfate (ZnSO₄)
Utilized in fertilizers, animal nutrition, pharmaceuticals, and industrial chemical manufacturing across multiple regulated industrial sectors.
Sodium Sulfate: (Na₂SO₄)
Used in detergents, glass manufacturing, textiles, and chemical processing industries supporting large-scale industrial and consumer product applications.
Oxides & Hydroxides
Calcium Oxide (Quicklime)
Used in metallurgy, construction, water treatment, and chemical processing for effective pH control and purification applications worldwide operations.
Calcium Hydroxide
Applied in water treatment, flue gas treatment, construction materials, and industrial chemical processes across infrastructure and applications.
Magnesium Oxide
Supports high-temperature reliability in refractories, environmental, pharmaceutical, industrial, and chemical applications.
Aluminum Oxide (Alumina)
Critical for ceramics, refractories, abrasives, and aluminum-related chemical processes requiring high purity, thermal stability, and performance.
Iron Oxide (Fe₂O₃)
Utilized in pigments, construction, metallurgy, and specialty applications supporting coloration, durability, corrosion resistance, and performance.
Titanium Dioxide: (TiO₂)
Widely used as a white pigment in coatings, plastics, paper, and chemical products requiring high brightness, opacity, and excellent stability.
Acids & Acid Derivatives
Sulfuric Acid (H₂SO₄)
A core industrial acid widely utilized across fertilizers, chemical synthesis, mineral processing, & essential battery manufacturing applications.
Hydrochloric Acid (HCl)
Primarily used for effective metal treatment, precise pH control, large-scale chemical synthesis, and various industrial cleaning processes.
Nitric Acid (HNO₃)
Frequently applied in the production of fertilizers, explosives, metal processing, and diverse specialty chemical manufacturing industrial sectors.
Phosphoric Acid (H₃PO₄)
Commonly used in agricultural fertilizers, food processing, water treatment facilities, and broad industrial chemical application sectors globally.
Sulfonic Acids (RSO₃H)
Essential key intermediates utilized in the formulation of detergents, surfactants, and various specialty chemical production processes globally.
Acid Recovery Streams
Recovered and recycled acids utilized within circular chemical processes to effectively reduce hazardous waste and total operating costs.
Mineral-Based Specialty Chemicals
Borax & Borates
Widely used in formulating detergents, glass manufacturing, advanced ceramics, and various specialty industrial application sectors globally today.
Perborates
Frequently applied as effective bleaching agents in laundry detergents and heavy-duty industrial cleaning formulations for optimal performance.
Silicates
Commonly used in detergents, robust construction materials, industrial adhesives, and diverse chemical processing applications across global markets.
Phosphates
Essential ingredients for agricultural fertilizers, municipal water treatment, food additives, and critical industrial manufacturing processes worldwide.
Carbonates
Extensively utilized in glass production, chemical synthesis, construction materials, and precise pH control applications in various industries.
Mineral Fillers
Used in plastics, paints, rubber, and construction products to significantly enhance material performance and improve overall cost efficiency.
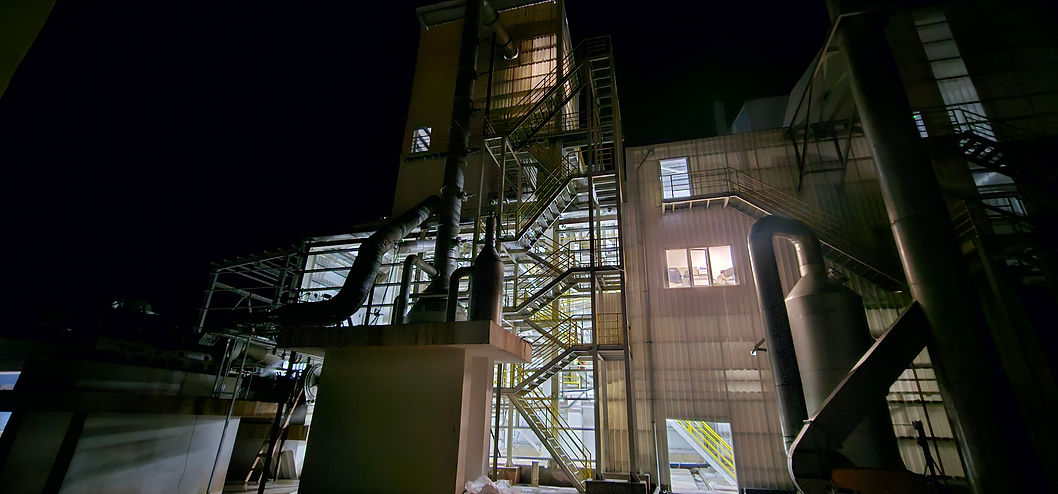
EPC & EPCM Solutions
Engineering & EPC Solutions for Inorganic & Mineral Chemical Plants
We provide complete EPC and EPCM solutions for inorganic and mineral chemical production facilities, covering process design, equipment selection, plant construction, commissioning, and operational support. Our solutions are designed to ensure consistent product quality, energy efficiency, environmental compliance, and long-term plant reliability.


bottom of page